


A container door opens and the first cartons release a stale, musty odour. Some sweatbands feel cool or slightly tacky. Paper inserts have softened. A few metal closures show early spotting. The commercial temptation is to blame a single cause—wet fabric, a bad desiccant pack, sea freight, or warehouse storage—but the smell alone does not identify where the water entered.
Moisture problems develop as a chain. Water may already be held in fabric or foam before sewing, added by humid finishing and packing conditions, trapped in bag air, absorbed by paperboard, or condensed when warm humid air meets a colder container surface. The practical task is to trace that chain and change the first controlling cause, not to hide the odour with fragrance or add more desiccant without evidence.
This guide is an operational framework for headwear buyers and factories. It does not prescribe universal moisture limits, desiccant quantities, exposure times or laboratory methods. Those controls must be defined for the actual materials, pack, route, season and customer requirement.
Start with the location of the symptom
A musty smell is an observation, not a root cause. Its location across cartons, colours and components helps narrow the mechanism before any units are aired, cleaned or redistributed.
Compare carton positions
Mark the container position, pallet, carton row and stack level when that information is available. A pattern near doors, walls, floor or roof suggests a different exposure path from an issue evenly distributed through all cartons. Connect the observation to the actual load arrangement in the carton load planning process.
Compare components inside the cap
Smell the shell, sweatband, foam, brim, mesh, label and packaging separately. A cotton shell, laminated front, synthetic mesh and paper insert can take up and release moisture at different rates. The strongest component signal may identify the main reservoir.
Compare opened and sealed units
Record whether odour appears immediately after opening a sealed bag, only after the cap warms, or mainly in cartons with damaged liners. Keep representative sealed units untouched. Opening every bag destroys the microclimate that may explain the problem.
Understand where water can enter
The shipment may contain water in several forms at once. Treat them as competing sources that need evidence, not as interchangeable labels.
Moisture held by materials
Textiles, foam, paperboard and natural-fibre trims can exchange water vapour with surrounding air. A material may look dry while still carrying more moisture than it will hold after reaching a drier warehouse. That release can raise humidity inside a sealed bag or carton.
Humidity added during production
Steam shaping, cleaning, spot treatment, screen-print curing, washing, air drying and humid weather can affect the condition at packing. Record when the last wet or heated process ended and how long the product rested before bagging.
Water introduced by packaging
Cartons, tissue, paper inserts and wooden pallets can arrive or be stored under damp conditions. They may become a source even when the cap itself entered packing in acceptable condition. Inspect packaging history as seriously as product history.
Condensation during transport
The official IMO/ILO/UNECE CTU Code includes an annex on prevention of condensation damage. Temperature cycles can move water vapour and create liquid water on colder surfaces. That transport mechanism must be considered alongside, not instead of, moisture already carried by the cargo and packaging.
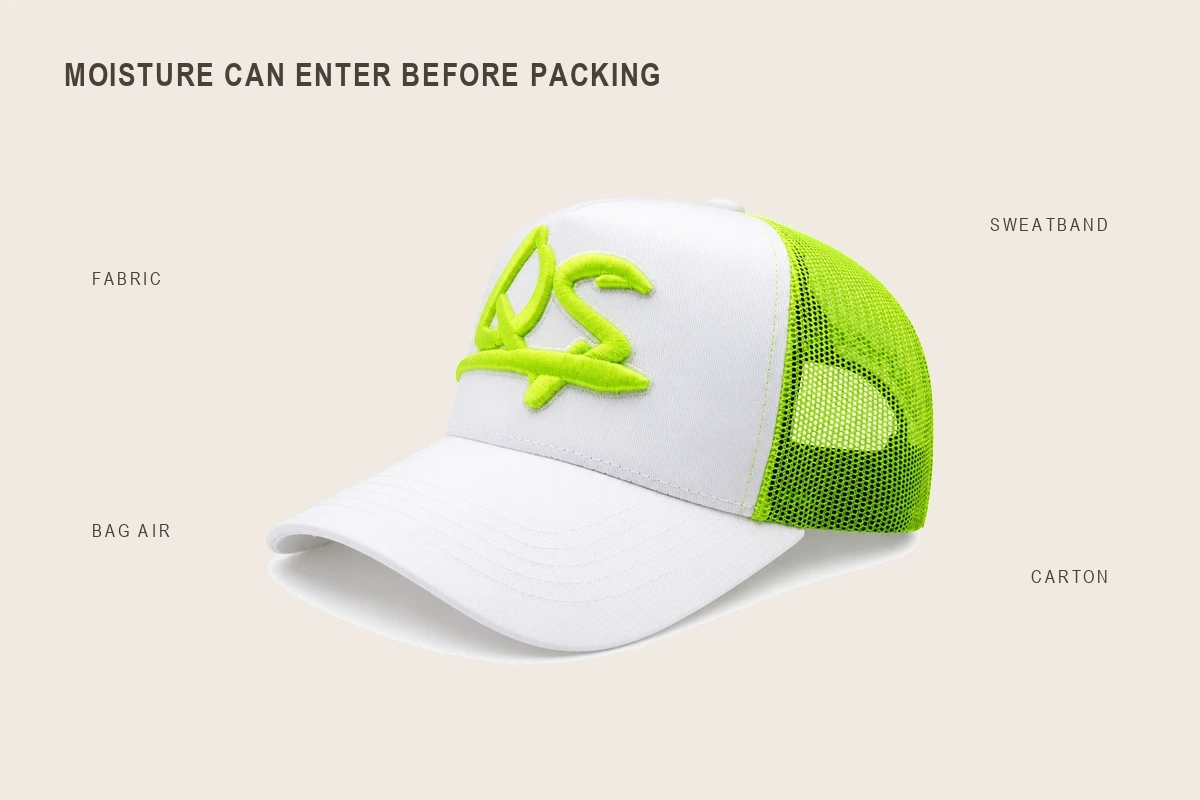
Read the cap as a moisture map
A cap combines materials with very different geometry and drying behaviour. Use the finished product to trace how moisture could collect, remain hidden or move.
Shell and laminated front
Structured fronts may combine outer fabric, adhesive, foam and backing. The surface can feel dry while internal layers release vapour more slowly. Compare odour and hand feel between structured and unstructured styles packed under the same conditions.
Sweatband and seam allowances
Sweatbands contain multiple folded layers and stitching channels. They are slower to inspect and may retain moisture near seams. Check coolness, tackiness, colour transfer, staining and odour without assuming each symptom has the same cause.
Mesh, closure and metal components
Open mesh may exchange air quickly, but adjacent foam or sweatband layers may not. Metal spotting can support an exposure pattern, yet a spot does not prove that container condensation caused the original textile odour. Keep observations separated until the pattern is clear.
Decoration and labels
Dense embroidery, patches, printed layers and labels add material and can slow local drying. Compare decorated and undecorated areas, especially where stitching creates closely packed layers.
Check the packing-room microclimate
The condition at the moment of sealing matters because the bag and carton preserve part of that environment.
Record conditions instead of describing the day
“It was humid” is not enough. Retain dated production and packing records from the actual location, together with the rest time between finishing and sealing. Use instruments and methods suitable for the facility and product; do not copy a limit from an unrelated programme.
Separate product conditioning from room air
A room can return to its target condition before thick or layered products do. Select representative caps from different operations and positions, not only one piece kept near the inspection desk.
Control the sealing sequence
If a warm or recently steamed cap is placed directly into a low-permeability bag, the local condition can differ from the room average. Document cooling, resting, bagging and carton closure as distinct steps.
Evaluate what each packaging layer does
Packaging can limit outside exposure, trap inside moisture, buffer humidity or become wet itself. The same layer can help in one route and hurt in another.
Polybag permeability and sealing
Define bag material, thickness, perforation and closure method. A fully sealed bag may preserve the packing microclimate, while a perforated bag exchanges air with the carton. Neither is automatically correct; the choice depends on product, route and channel protection needs.
Paperboard absorption
Cartons and inserts can absorb water during storage, loading and transit. The CTU Code guidance on packing and moisture-protection materials discusses protection against condensed humidity and the use of separation or ventilation gaps in appropriate situations. A headwear pack still requires route-specific validation.
Desiccant as capacity, not decoration
A desiccant pack has finite capacity and needs a defined use case. More packets do not correct wet products, damp cartons, an unsuitable bag system or uncontrolled storage. Obtain supplier data for the actual desiccant and calculate against the pack and route instead of adopting a generic count.
Spacing and contact with container surfaces
Carton contact with floor, walls or roof can change exposure. Load layout, dunnage and movement controls should be agreed with qualified logistics parties. The goal is not to turn the product team into container engineers, but to connect cap symptoms with real stowage evidence.
Inspect the container and warehouse handoff
Evidence at receipt can disappear quickly once doors remain open, cartons move and air conditions change.
Document before ventilation changes the scene
Record door condition, seals, visible droplets, stains, odour intensity by area, carton surfaces and product state as soon as safe access is established. Use the controlled evidence principles in the technical support escalation process.
Separate active water from historic exposure
A dry carton with staining may show an earlier event; a cool damp carton may show current exposure. Photograph both product and packaging, then retain representative samples rather than discarding packaging immediately.
Review destination storage
Goods can be acceptable at discharge and change during warehouse storage. Record unloading weather, dwell time, pallet wrapping, wall clearance and warehouse conditions. Do not assign the complete cause to ocean transit without checking the destination handoff.
Run comparisons that isolate the mechanism
A useful investigation changes one factor at a time. The aim is to discover which condition changes the outcome, not to produce a large photo folder.
Compare controlled samples
Use the same SKU and production lot where possible. Compare sealed versus ventilated packs, different carton positions, packaging lots, decoration types or finishing times. Keep the comparison small enough to interpret.
Use an appropriate inspection sample
The headwear sampling and defect framework explains lot identity and representative selection. For a moisture investigation, add targeted observations without automatically treating a pre-shipment AQL plan as the contractual basis for an arrival claim.
Record both positive and negative findings
If a dry carton, unaffected colour or different decoration stays acceptable, retain that evidence. Negative findings narrow the mechanism and prevent the team from blaming every material in the specification.
Decide what can be recovered
Not every musty cap requires disposal, and not every unit is safe to release after airing. Recovery depends on cause, severity, material response, appearance, channel requirements and evidence.
Hold stock until the cause is understood
Separate released, quarantined, trial-recovery and rejected units. Avoid mixing aired units back into sealed stock before the team can compare them.
Trial the least invasive action
Controlled ventilation, conditioning or packaging replacement may help some cases, but the repaired product must be reassessed for odour, appearance, function, staining and decoration. Do not mask odour with fragrance.
Escalate visible growth or uncertain safety
Suspected mould, significant staining or uncertain contamination needs competent technical review. This article does not provide a release threshold. Protect workers and customers and follow applicable product, workplace and disposal requirements.
Connect commercial settlement only after the evidence
If nonconformity is confirmed, the bulk-cap claim settlement guide compares replacement, credit and controlled rework. Keep the mechanism investigation and commercial negotiation connected but distinct.
Change the first controlling cause
Corrective action should target the earliest verified point that controls the downstream condition. Adding controls at every step increases cost without proving which one works.
If materials enter packing too wet
Define material receipt, storage and pre-packing conditioning for the actual construction. Include layered components, not only shell fabric. Verify the change through representative product rather than a room reading alone.
If the packing sequence traps moisture
Change rest, cooling, bagging or carton-close timing and run a controlled pack comparison. Update operator instructions only after the trial shows a repeatable improvement.
If packaging becomes the source
Control carton and insert storage, incoming condition and protection during packing. Connect packaging choices to the existing retail carton and pack-out requirements so moisture control does not remove necessary channel protection.
If the route creates condensation exposure
Review pack permeability, moisture capacity, stowage, dunnage and route conditions with the packaging and logistics providers. Confirm the current solution for the actual lane rather than copying a previous desiccant or liner specification.
Write moisture control into the next order
The lesson should become measurable purchasing and production inputs, not a warning in an email thread.
Define observable pack evidence
Record the product revision, packaging materials, sequence, representative condition readings, carton identity and approver. Avoid a generic “keep dry” note that no one can execute or verify.
Add focused release checks
Check carton and packaging condition, product odour and agreed risk components before shipment. If the order serves a retailer, connect final carton execution to the retail receiving evidence.
Revalidate when construction or route changes
A new foam, sweatband, bag, carton, season, warehouse or shipping lane changes the moisture system. Revalidate the relevant steps instead of assuming the old pack remains safe.
Trace the water before choosing the fix
Musty headwear is not solved by one universal humidity number or a standard packet count. Locate the symptom, identify the water sources, compare components and carton positions, reconstruct the packing and route microclimate, then test the smallest change that controls the mechanism.
The fastest useful question is not “How do we remove the smell?” It is “Where did the water enter, where was it stored, and what prevented it from leaving?” Answer that well, and the next order can carry a specific control rather than another assumption.





